 Tel: +86 13342660375
 E-mail:

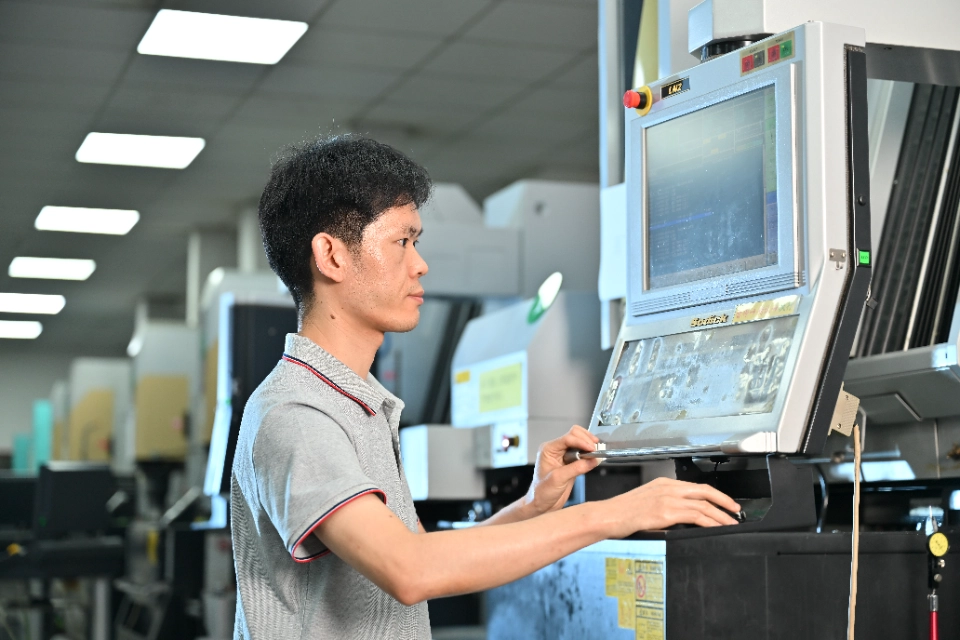
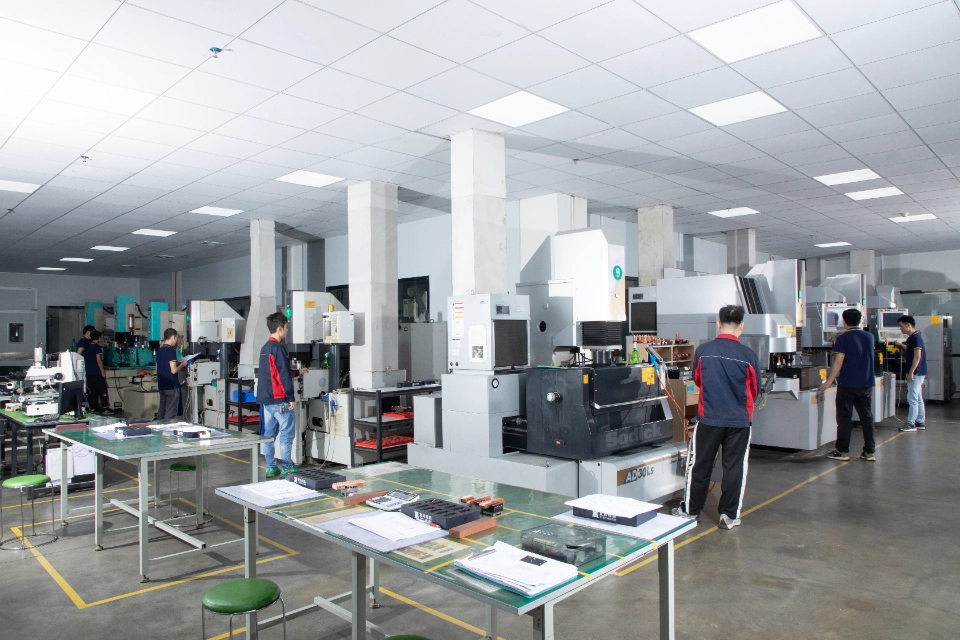
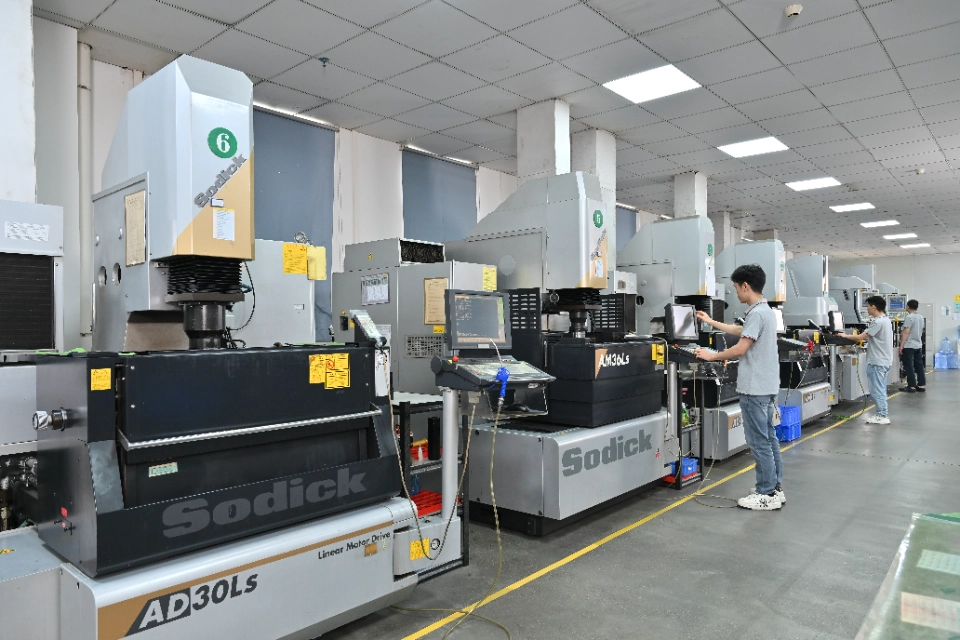


Our EDM workshop is equipped with multiple Sodick AD30Ls CNC die-sinking electrical discharge machines. The model markings visible in the workshop identify the equipment as the AD30Ls series, while the control panel uses Sodick’s LN2 CNC system.
Sodick classifies the AD30Ls as a linear-motor-driven, high-speed die-sinking EDM machine. It is used in our factory for machining precision mold cavities, deep ribs, narrow slots, internal corners, and other detailed features that are difficult to produce with conventional cutting tools.
Key Advantages:
- Precision cavity machining
- Complex internal geometries
- Low mechanical cutting force
- Controlled surface finishing
- Stable repeat production
Equipment and Production Capabilities
The Sodick AD30Ls removes material through controlled electrical discharges between a shaped electrode and an electrically conductive workpiece. Because the electrode does not mechanically cut the material, the process is suitable for hardened steel, tool steel, carbide, and other conductive materials that may be difficult to machine after heat treatment.
In our factory, the equipment is mainly used for:
- Precision mold inserts and cores
- Deep cavities and narrow ribs
- Connector mold components
- Complex recesses and internal profiles
- Sharp internal corner features
- Hardened tooling components
- Components requiring detailed surface textures
Copper or graphite electrodes are prepared according to the required component geometry. Different electrodes may be used for rough machining, semi-finishing, detailed feature machining, and final surface finishing.
The linear-motor drive structure used by Sodick die-sinking EDM systems supports responsive axis movement without a conventional ball-screw transmission mechanism. Sodick’s current AD-series documentation also describes linear motor drives, glass-scale feedback, dielectric-fluid temperature control, and discharge circuits intended to support stable precision machining and fine surface generation.
Role in Our EDM Workshop
Several Sodick EDM machines are arranged within the same production area, allowing our team to allocate work according to cavity size, electrode quantity, material condition, surface requirements, and production schedule.
The equipment is integrated into our internal mold and precision-component workflow. CNC programming, electrode preparation, fixture setup, EDM machining, and dimensional inspection are coordinated by our own engineering, machining, and quality teams.
A typical production sequence may include:
- CNC rough machining of the workpiece
- Heat treatment when required
- Copper or graphite electrode machining
- Sodick die-sinking EDM
- Dimensional and profile inspection
- Polishing or final finishing
Keeping these processes within the same factory helps our team adjust electrode offsets, discharge parameters, machining depths, and finishing allowances according to inspection results.
The LN2 controller visible in the image supports CNC programming and coordinated discharge machining. Sodick documentation for LN2-equipped die-sinking EDM systems lists linear-motor control, linear-scale position detection, multi-axis control, and fine command resolution as part of the control platform.
The Sodick AD30Ls machines shown are part of our factory’s precision mold and EDM manufacturing capability. Actual processing results depend on the electrode design, workpiece material, cavity depth, surface-finish requirement, fixture stability, and inspection standard for each component.
Contact Information
-
 [email protected]
-
 +86 13342660375Telephone
-
 Address
No. 62, Jinghai East Road, Shatou Community, Chang' an Town, Dongguan City, Guangdong Province, China
 Schedule a Home Visit
Leave us a Message
Have questions or need assistance? Get in touch with us, and we’ll be happy to help!


