 Tel: +86 13342660375
 E-mail:



- Main Product: Custom POM+PA Automotive Electrical Connector & Terminal Carrier Multi-Cavity Injection Mold
- Machining Precision: ±0.002mm ultra-precision dimensional control
- Optional Materials: Corrosion-resistant high-hardness mold steel (S136H, STAVAX, 2344)
- Processing Technology: 5-axis CNC milling, sinker EDM, wire cut WEDM, precision grinding, vacuum heat treatment, automotive standard texture etching
- Product Features: Modular interchangeable cavity layout, POM-PA dedicated textured cavity, independent partition cooling channels, multi-slide thin pin core pulling structure, anti-deformation heavy-load mold frame, multi-color housing compatible molding system
Detailed Introduction
This precision multi-cavity injection mold is professionally developed for automotive electrical system plastic structural parts, fully adjusted for POM-PA alloy plastic’s unique melt fluidity, low shrinkage and self-lubricating properties, meeting automotive electronic standards of abrasion resistance, insulation and long-term vibration stability.
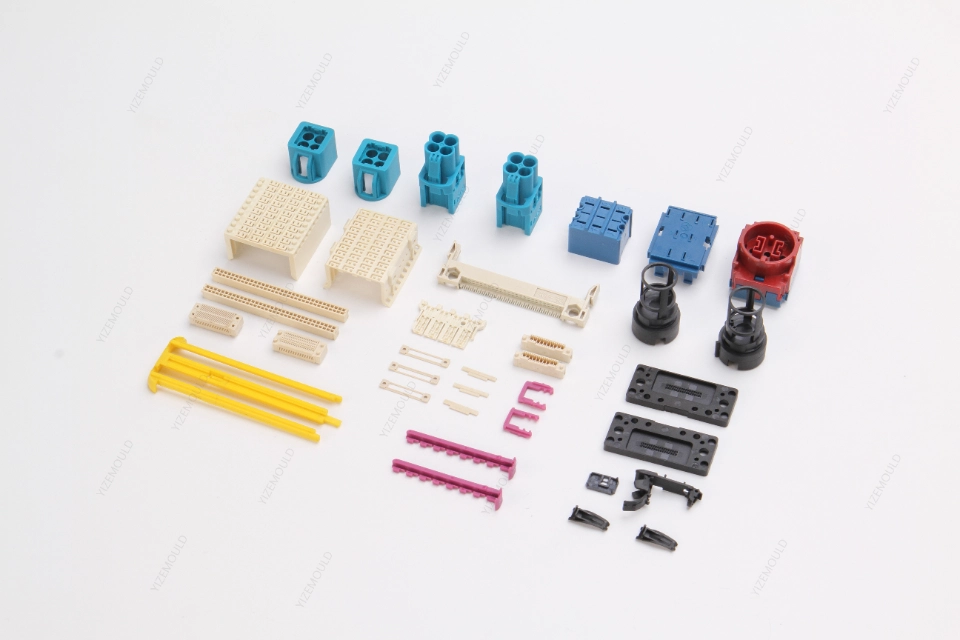
The mold adopts standard two-plate fixed-moving split structure, supporting independent cavity customization for all components shown in the picture: multi-hole high-current connector bases, dense pin terminal strips, long positioning guide bars, miniature locking buckles and circuit board mounting brackets. Each functional component cavity is an independent embedded insert, which can be quickly replaced to switch different pin-count connector models, reducing repeated mold development costs for multi-product production lines. All molding surfaces adopt uniform matte automotive texture etching, effectively covering micro flow marks and gloss unevenness easily generated during POM-PA injection molding, eliminating secondary surface trimming process.
Independent distributed cooling pipelines are laid out for every single cavity, which accurately balance mold temperature during continuous injection of POM-PA alloy plastic, greatly restrain internal stress, long strip warpage and uneven shrinkage caused by inconsistent cooling rate of POM and PA base materials. Multi-direction thin-slide side core pulling mechanism is integrated to form dense terminal pin slots, undercut locking structures and multi-passage plug cavities in one molding cycle. Precision interlock slide locking blocks maintain stable clamping force under long-cycle continuous production, prevent flash on ultra-thin wall latch and tiny pin slot structures, and extend mold service life under long-term POM-PA cyclic molding.
Complete Precision Machining Workflow
- 5-axis CNC rough milling for mold base outline and cavity rough forming
- Vacuum stress relief heat treatment to stabilize steel hardness, reduce thermal deformation under long-term POM-PA cyclic injection molding
- Precision surface grinding to control mold plate flatness and parallelism within ±0.002mm
- Sinker EDM & wire cut WEDM for ultra-fine thin-wall latch, dense pin slot and multi-port connector contour features
- Automotive-grade uniform texture etching, optimized surface finish matching POM-PA melt fluidity
- Optional non-toxic anti-corrosion surface coating compatible with POM-PA alloy automotive engineering plastics
All mold core, cavity and structural components complete full 3D coordinate measurement inspection to meet strict automotive electronic drawing tolerance standards. Full customization is supported based on customer connector samples or 2D/3D engineering drawings: cavity quantity, mold steel grade, cooling channel layout and texture depth can be adjusted according to POM-PA blending ratio, vehicle IP protection grade and daily production capacity. The modular interchangeable multi-cavity layout significantly improves molding flexibility while unifying dimensional consistency and surface quality of all types of automotive electrical connector accessories.
Specification Table
| Item | Details |
| Product Name | Custom Multi-Cavity POM+PA Automotive Electrical Connector & Terminal Carrier Injection Mold |
| Core Structure | Split fixed & moving mold plates, modular interchangeable multi-cavity layout, independent replaceable connector cavity inserts, multi-direction thin-slide side core pulling, precision interlock locking mechanism, full distributed independent segmented cooling flow channels, heavy-load four guide pin positioning columns |
| Machining Tolerance | ±0.002mm geometric tolerance (flatness, parallelism, thin-wall buckle & dense pin slot contour precision) |
| Optional Mold Steel | Automotive grade S136H, STAVAX corrosion-free pre-hardened mold steel, high-temperature resistant 2344 alloy mold steel |
| Manufacturing Process | 5-Axis CNC Milling, Precision Surface Grinding, Sinker EDM, Wire Cut WEDM, Vacuum Stress Relief Heat Treatment, Automotive Standard Texture Etching, Optional Non-Toxic Anti-Corrosion Coating |
| Product Advantages | Customized per automotive connector 2D/3D drawings, POM-PA optimized textured cavity to eliminate flow lines & sink marks, independent cooling to restrain material differential shrinkage & long strip warpage, detachable inserts for fast model switching, multi-slide core pulling for dense pin & undercut structures, stable slide locking to avoid thin-wall flash, abrasion-resistant mold surface matching self-lubricating POM-PA, high-volume multi-cavity mass production performance |
| Application Fields | POM+PA automotive wiring harness connector housing injection molding, new energy vehicle signal & low-current connectors, ECU terminal carrier strips, automotive instrument small plastic locking parts, vehicle power distribution module positioning brackets, commercial vehicle electrical plug auxiliary fittings |
Contact Information
-
 [email protected]
-
 +86 13342660375Telephone
-
 Address
No. 62, Jinghai East Road, Shatou Community, Chang' an Town, Dongguan City, Guangdong Province, China
 Schedule a Home Visit
Leave us a Message
Have questions or need assistance? Get in touch with us, and we’ll be happy to help!


